


A practical engineering guide from Fortune Wheel Parts on why aluminum wheels require a different lug nut spec than steel wheels, covering galvanic corrosion, seat geometry, thread engagement, and torque settings.
- Aluminum wheels need different lug nuts for two reasons: galvanic corrosion and seat geometry. A steel lug nut on an aluminum wheel creates a galvanic cell in the presence of road moisture, and the aluminum wheel is the metal that corrodes.
- Match the seat geometry to the wheel. The most common aluminum-wheel seat is the 60 degree conical seat (also called acorn); other geometries are ball and flat. Mismatched seats will crack the wheel in 10-20 install cycles.
- Aluminum wheels are tightened to a lower torque than steel wheels — typically 80-120 ft-lb (108-163 Nm) versus 100-150 ft-lb (136-203 Nm) for steel — because of the lower yield strength of the aluminum alloy.
- Two-piece lug nuts give more accurate torque readings than one-piece because the cap decouples the socket from the wheel contact surface, which is critical on shallow aluminum wheel seats.
- Minimum thread engagement equals the stud diameter (12 mm for M12, 14 mm for M14); under-engagement is the most common cause of stud shear in service.
Direct answer up front: Aluminum wheels need a different lug nut specification than steel wheels for two engineering reasons. First, when a steel lug nut contacts an aluminum wheel seat in the presence of road moisture, the two metals form a galvanic cell and the aluminum wheel corrodes preferentially — even when the lug nut is still tight, the wheel seat pits, the clamp force drops, and the failure mode is usually a cracked wheel around the lug hole. Second, aluminum wheel seats are shallower and more precisely machined than steel wheel seats, so they require a matching seat geometry (60 degree conical, ball, or flat) and a lower torque value (typically 80-120 ft-lb / 108-163 Nm) than the 100-150 ft-lb / 136-203 Nm typical of a steel wheel. Get the seat, the torque, and the thread engagement right, and the aluminum wheel will outlast the steel one; get any of the three wrong, and the wheel is the first thing to fail.
I have spent most of my career in the wheel service parts business at Fortune, which has been making wheel balance weights, tire valves, and tool accessories since 1996. The most common question our customer service team fields from distributors and fleet buyers is some version of “I bought lug nuts from you, why are my wheels cracking?” The answer is almost always one of the three: wrong seat, wrong torque, or wrong thread engagement. This article walks through each of the three, and the questions to ask the supplier before you commit to a part number.

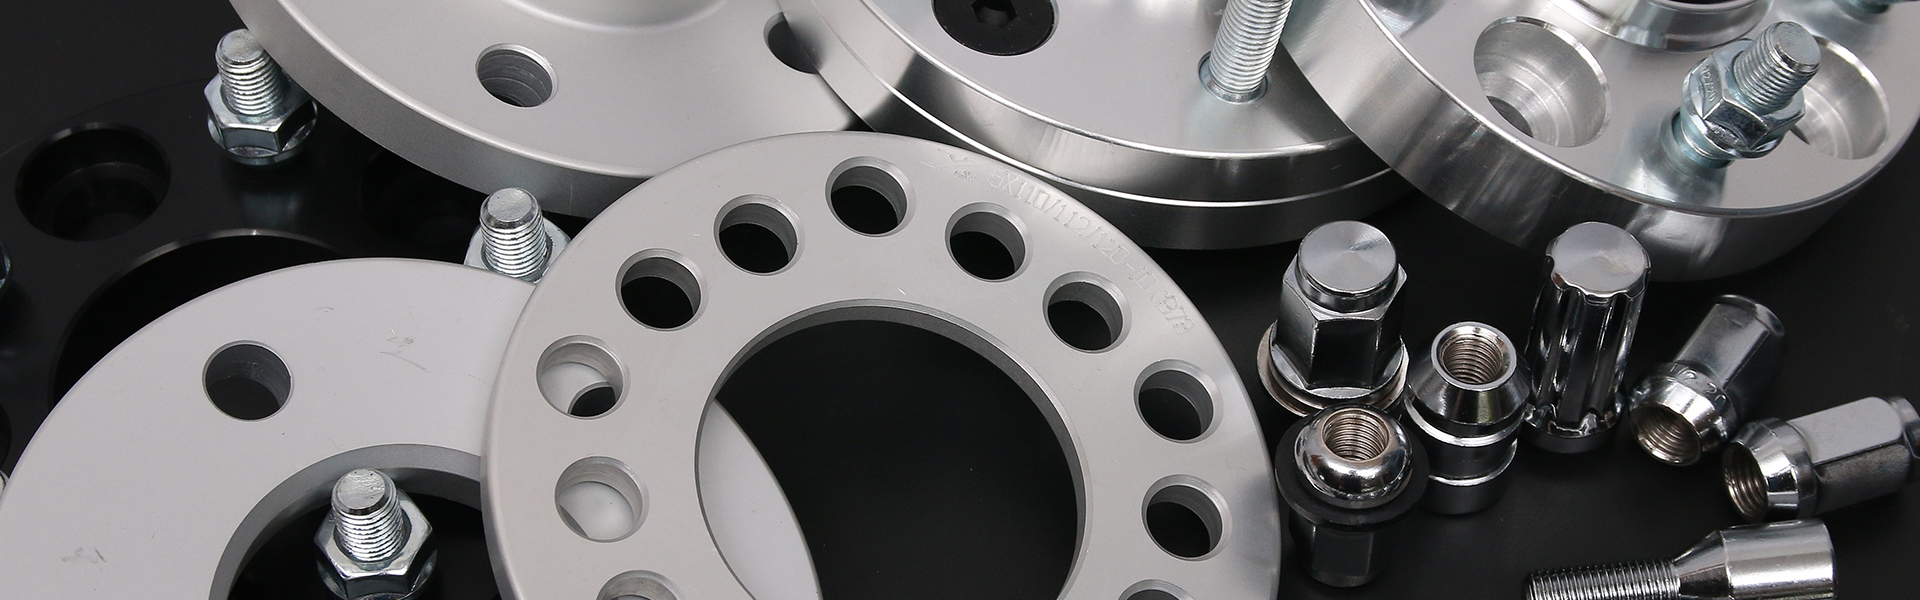
Two-piece 60 degree conical seat lug nuts (13/16″ hex, 1.26″ overall length) for aluminum racing wheels. Image: fortunewheelparts.com / Fortune Wheel Parts.
What Makes Aluminum Wheel Lug Nuts Different from Steel Wheel Lug Nuts?
Two engineering factors, and they both show up in the first service interval. The first is the metallurgical factor — the galvanic corrosion that occurs when a steel fastener contacts an aluminum wheel in the presence of any electrolyte, which on a road vehicle is always present in the form of moisture, road salt, or humid air. The second is the geometric factor — the aluminum wheel seat is shallower and more precisely machined than a steel wheel seat, so the lug nut seat angle and the lug nut open-end length have to match the wheel within tight tolerances.
Most aluminum wheel failures attributed to “bad lug nuts” are actually caused by one of these two factors. The lug nut looks fine, the threads look fine, the torque wrench clicked at the right value — but the wheel seat is pitted from galvanic corrosion, or the seat geometry is mismatched by five degrees, or the lug nut open-end length is too short for the stud to engage properly. The failure shows up later, on the highway, when the clamp force finally drops below what the wheel needs to stay seated.
Diagnosis (Answer Nugget): Aluminum wheels need different lug nuts than steel wheels for two reasons: the galvanic corrosion that occurs at a steel-on-aluminum interface in the presence of moisture, and the tighter geometric tolerance required by the shallower, more precisely machined aluminum wheel seat.
What Is Galvanic Corrosion and How Does It Affect a Lug Nut and Wheel Interface?
Galvanic corrosion is the electrochemical reaction that occurs when two dissimilar metals are in electrical contact in the presence of an electrolyte. The metal that is more electrochemically active (higher in the galvanic series, also called the more “anodic” metal) loses electrons and corrodes; the metal that is less active (the more “cathodic” metal) gains electrons and is protected.
Aluminum and steel are far apart in the galvanic series. Aluminum is the more active metal — it is the anode — and it corrodes preferentially when paired with steel. On a vehicle, the steel stud or lug nut is the cathode (protected), and the aluminum wheel is the anode (corroded). The corrosion shows up first as a white or gray powdery deposit on the wheel seat, then as pitting of the aluminum surface, and finally as a loss of clamp force as the wheel material disappears from under the lug nut seat.
The reaction needs three things to proceed: two dissimilar metals, an electrical path between them (the contact between the stud, the lug nut, and the wheel seat provides this), and an electrolyte (road moisture, road salt, and humid air are all sufficient). On a road vehicle, all three are present every time it rains. The reaction rate accelerates in coastal environments, in winter road-salt service, and in any climate where the vehicle sits outside between drives.
Galvanic mechanism (Answer Nugget): Galvanic corrosion at a steel-on-aluminum interface requires two dissimilar metals (steel and aluminum), an electrical path (the stud-to-wheel contact), and an electrolyte (road moisture or road salt). The aluminum corrodes preferentially; the steel is protected. Pitting of the wheel seat, loss of clamp force, and eventual wheel failure follow.
The standard mitigation is to ensure the wheel-contacting surface of the lug nut is plated with a compatible material — zinc, chrome, or a black Dacromet-style coating — and to keep the contact area clean. For service fleets, an annual inspection of the wheel seat and a re-torque to the wheel manufacturer’s spec is the cheapest insurance against a galvanic-related wheel failure.
What Seat Geometry Should I Use on an Aluminum Wheel?
The seat is the part of the lug nut that physically contacts the wheel around the lug hole. Three seat geometries cover the majority of aluminum wheels in service today.
60 Degree Conical Seat (Acorn)
The 60 degree conical seat — also called the acorn seat or the tapered seat — is the most common aluminum-wheel seat. The lug nut is shaped like an acorn (hence the nickname), with a 60 degree taper on the wheel-contacting surface. When the lug nut is tightened, the taper centers the wheel on the stud and clamps the wheel seat to the lug nut seat along a continuous ring. The 60 degree geometry is used by most North American and Japanese OEM aluminum wheels, and it is the standard geometry in the Fortune wheel lug nuts and bolts product range, including the racing-car 2PC BULGE ACORN part numbers 1702, 1704, 1706, 1707, 1709, 1712, and 1714.
Ball Seat
The ball seat uses a spherical contact surface (a section of a sphere) instead of a cone. The ball seat is common on European OEM aluminum wheels, particularly on German vehicles. The contact area is a narrow ring at the equator of the sphere, which gives a more accurate centering of the wheel on the stud at low torque. The ball seat cannot be interchanged with a conical seat — the geometries look similar but clamp very differently.
Flat Seat (Mag Seat)
The flat seat — sometimes called the mag seat — uses a flat washer face on the lug nut to clamp against a flat counterbore on the wheel. The flat seat is common on aftermarket aluminum wheels and on some European and Japanese applications. The flat seat requires higher torque than the conical seat to achieve the same clamp force, and is more sensitive to surface finish on the wheel counterbore.
| Seat Type | Geometry | Common Application | Cross-Compatibility |
|---|---|---|---|
| 60 degree conical (acorn) | 60 degree taper | Most North American and Japanese OEM aluminum wheels | Not interchangeable with ball or flat |
| Ball | Spherical contact | Many European OEM aluminum wheels | Not interchangeable with conical or flat |
| Flat (mag) | Flat washer face | Aftermarket aluminum, some European and Japanese | Not interchangeable with conical or ball |
What Torque Setting Should I Use on an Aluminum Wheel?
The honest answer is the same as it has been for the past thirty years: follow the wheel manufacturer’s torque specification, not the vehicle manufacturer’s. The wheel manufacturer designs the wheel to a specific clamp force at a specific lug-nut torque, and that torque value is on the wheel manufacturer’s documentation (often printed on the wheel box, in the wheel installation guide, or in the wheel maker’s online fitment database).
For a typical cast or flow-formed aluminum wheel in the 15-22 inch diameter range, the torque spec falls in the 80-120 ft-lb (108-163 Nm) range. Forged aluminum wheels can sometimes accept a slightly higher torque because of the higher material strength, but the wheel maker still has the final say. A steel wheel of the same diameter typically takes 100-150 ft-lb (136-203 Nm).
The lower torque on aluminum wheels reflects two engineering realities. First, the yield strength of the typical cast aluminum alloy used in wheels is roughly 30-50 percent of the yield strength of the steel used in lug nuts, so the wheel is the weaker link in the clamp system. Second, the aluminum wheel seat is shallower than the steel seat, so over-torque stretches the stud before the wheel seat is fully clamped.
The other thing the torque spec assumes is the install procedure. The lug nuts should be tightened in a star (criss-cross) pattern, in two or three stages — typically 50 percent, 80 percent, and 100 percent of the final torque — to seat the wheel evenly against the hub. A single-stage torque to the final value on a wheel that has not been pre-seated will distort the wheel and leave some lugs under-clamped and others over-clamped. The install procedure is half the torque spec; ignore it and the torque value on the page is meaningless.
Torque rule (Answer Nugget): Use the wheel manufacturer’s torque specification, not the vehicle manufacturer’s, and tighten in a star pattern in two or three stages to 50 / 80 / 100 percent of the final value. Aluminum wheels are typically tightened to 80-120 ft-lb (108-163 Nm); over-torque will crack the wheel and stretch the stud.
Are Two-Piece Lug Nuts Better Than One-Piece for Aluminum Wheels?
For aluminum wheels, two-piece lug nuts are the better choice. The two-piece design splits the lug nut into a separate cap (which the socket contacts) and a base (which contacts the wheel). The cap decouples the socket from the wheel-contacting surface, which means the torque reading on the wrench reflects only the force needed to clamp the wheel, not the friction between the socket and the cap. The result is a more accurate torque value and a more consistent clamp force from one lug nut to the next.
Two-piece lug nuts also let the cap and the base be specified in different materials. The base can be zinc-plated steel (compatible with aluminum wheels and corrosion-resistant), and the cap can be chrome-plated for appearance. The Fortune racing-car racing car wheel lug nuts with 60 degree conical seat are a 2-piece design with chrome or black surface treatment options, and the documented 1.26″ overall length and 13/16″ hex match the typical aluminum racing-wheel specification.
One-piece lug nuts are cheaper to manufacture and they work, but the socket contacts the same surface that contacts the wheel, which means the torque reading is contaminated by the socket-to-nut friction. On a steel wheel, the contamination is small enough to be ignored. On an aluminum wheel, where the seat surface is shallow and easily distorted, the contamination can be the difference between a wheel that stays seated and a wheel that does not.
How Much Thread Engagement Do I Need?
The minimum thread engagement rule is the easiest of the aluminum-wheel specifications to get right and the easiest to get wrong. The rule is: the lug nut should engage the stud by at least the same number of thread pitches as the stud diameter. For an M12 x 1.5 stud, that is 12 mm of engagement. For an M14 x 1.5 stud, that is 14 mm. For a 7/16-20 stud (the common North American thread size), that is 7/16 inch, or roughly 11 mm.
The lug nut open-end length should be at least equal to the stud diameter. For an M12 stud, the open-end length should be at least 12 mm. For a 2-piece lug nut, the open-end depth of the base is the controlling dimension, not the overall length of the assembled lug nut. Insufficient thread engagement is the most common cause of stud shear during service, and it is almost always caused by an open-end length that is too short for the stud.
The way to check engagement before installation is to thread the lug nut onto the stud by hand, and confirm that at least the specified number of thread pitches are engaged with no cross-threading. The visual check is fast, and it catches the problem before the wheel is on the ground.
Do I Need Anti-Seize on Aluminum Wheel Lug Nuts?
Yes, with one important caveat. A small amount of copper-based or nickel-based anti-seize on the stud threads is good practice on aluminum wheels, for two reasons. First, it prevents thread galling between the steel stud and the steel lug nut, which is a particular problem on fine-pitch studs (M12 x 1.5, M14 x 1.5) where the threads can cold-weld under high clamp force. Second, it gives a more consistent torque reading by stabilizing the friction at the thread interface.
The caveat is that anti-seize must not be applied to the wheel-contacting seat surface. Anti-seize on the seat changes the friction at the seat interface, which invalidates the torque value the wheel manufacturer specified. The wheel manufacturer’s torque assumes a clean, dry, unlubricated seat, and a lubricated seat will read the same torque on the wrench but deliver a much higher clamp force on the wheel. The result is over-clamping, wheel distortion, and (again) a cracked wheel.
The correct application is anti-seize on the stud threads only, with the seat surface cleaned and dry. If the wheel and lug nut manufacturer specify a particular lubricant (some racing applications call for a specific thread paste), follow their guidance.
How Do I Match the Fortune Range to an Aluminum Wheel?
The Fortune racing-car 2PC BULGE ACORN range covers seven thread sizes across the most common North American and international stud specs: 7/16, 1/2, 12mm x 1.25, 12mm x 1.50, 12mm x 1.75, 14mm x 1.50, and 14mm x 2.00. The 13/16 inch hex and 1.26 inch overall length are consistent across the range, so the only selection variables are the thread size and the surface treatment (chrome or black).
For a fleet or service application, the right approach is to build a compatibility matrix that ties each part number to the specific wheel model it is approved for, and to keep the matrix with the install documentation. The matrix should also note the wheel manufacturer’s torque spec, the required star-pattern tightening sequence, and the thread-engagement check. The matrix turns the install procedure from a per-mechanic judgment into a per-vehicle specification, which is the difference between a wheel service that prevents failures and a wheel service that has them.
If you are not sure which part number fits which wheel, the easiest path is to request aluminum wheel lug nut technical consultation from the Fortune engineering team. Send the wheel model, the stud thread size (or the vehicle make and model if the stud size is not known), and the surface treatment preference, and the team will come back with a part number, the torque spec, and the install procedure within a working day.
Need Help Specifying Lug Nuts for an Aluminum Wheel?
Send the wheel model, the stud thread size, and the surface treatment preference. The Fortune engineering team will come back with a part number, the torque spec, and the install procedure within one working day.
Frequently Asked Questions
Why do aluminum wheels need different lug nuts than steel wheels?
Aluminum wheels need different lug nuts for two main reasons. First, when a steel lug nut sits against an aluminum wheel seat, the two dissimilar metals form a galvanic cell in the presence of road moisture and road salt, and the aluminum wheel corrodes preferentially. Second, aluminum wheel seats are typically shallower and more precisely machined than steel wheel seats, so they require a matching seat geometry (60 degree conical, ball, or flat) to clamp correctly without cracking the wheel.
What is galvanic corrosion and how does it affect a lug nut and wheel interface?
Galvanic corrosion is the electrochemical reaction that occurs when two dissimilar metals are in electrical contact in the presence of an electrolyte. Road moisture, road salt, and humid air all act as electrolytes at the wheel-fastener interface. The metal higher in the galvanic series (in this case the aluminum wheel) acts as the anode and corrodes preferentially, while the metal lower in the series (the steel lug nut) is protected. The result is pitting, material loss at the wheel seat, and eventual loss of clamp force even when the lug nut is still tight.
What seat geometry should I use on an aluminum wheel?
Match the seat geometry on the lug nut to the seat geometry on the wheel. The most common aluminum-wheel seat is the 60 degree conical seat (also called acorn or tapered). Other common geometries are the ball seat (used on many European vehicles) and the flat / mag seat (used on some aftermarket wheels). Mismatched seats clamp unevenly, distort the wheel, and will crack the wheel around the lug hole in as few as 10-20 install cycles.
What torque setting should I use on an aluminum wheel?
Always follow the wheel manufacturer’s torque specification, not the vehicle manufacturer’s. Aluminum wheels are typically tightened in the 80-120 ft-lb (108-163 Nm) range, well below the 100-150 ft-lb (136-203 Nm) typical of a steel wheel. The lower torque reflects the lower yield strength of the aluminum alloy compared to steel. Over-torquing an aluminum wheel stretches the stud, can crack the wheel, and makes future removal difficult.
Are two-piece lug nuts better than one-piece for aluminum wheels?
Two-piece lug nuts (a separate socket-contacting cap and a base that contacts the wheel) give more accurate torque readings than one-piece designs, because the cap decouples the socket from the wheel contact surface. The two-piece design also lets the cap and the base be finished in different materials (chrome cap, zinc-plated base), so the wheel-contacting surface can be specified to minimize galvanic risk while the visible cap can be chrome-plated for appearance. For racing and high-vibration service, two-piece is the safer choice.
Can I re-use lug nuts when I rotate tires?
Re-use is acceptable when the lug nut is the correct spec for the wheel, the threads and the seat are clean and undamaged, and the torque is applied with a calibrated wrench to the wheel manufacturer’s specification. Lug nuts that show signs of corrosion, thread galling, deformed seats, or rounded hex corners should be replaced. Aftermarket aluminum lug nuts typically have a 3-5 year service life; steel lug nuts in the same service have a longer life but introduce a galvanic risk on aluminum wheels.
What thread engagement length do I need on an aluminum wheel?
For an aluminum wheel, the stud should engage the lug nut by at least the same number of thread pitches as the stud diameter. For an M12 x 1.5 stud, that is 12 mm of thread engagement; for an M14 x 1.5 stud, 14 mm. The lug nut open-end length should be at least equal to the stud diameter, and for two-piece designs, the open-end depth of the base should be the controlling dimension. Insufficient thread engagement is the most common cause of stud shear during service.
Do I need to use an anti-seize compound on aluminum wheel lug nuts?
A small amount of copper-based or nickel-based anti-seize on the stud threads is good practice on aluminum wheels, because it prevents thread galling between the steel stud and the lug nut and gives a more consistent torque reading. Do not apply anti-seize to the wheel-contacting seat surface, because the compound changes the friction at the seat and invalidates the torque spec. Follow the wheel and lug nut manufacturer’s guidance if a specific lubricant is recommended.
How do I know if a lug nut is rated for aluminum wheels?
The lug nut should be marked or documented by the manufacturer as suitable for the wheel material and seat geometry, with a specified torque value and a specified stud engagement length. The Fortune racing-car lug nut range is documented for 60 degree conical seat aluminum wheels with 13/16 inch hex across the listed part numbers. For a fleet or service application, ask the supplier to provide a compatibility matrix that ties each part number to specific wheel models, rather than relying on the generic ‘fits most’ marketing language.
Reference Standards & Authoritative Sources
The galvanic corrosion framework, torque specification practice, and thread engagement rules referenced throughout this article are drawn from the following international standards bodies and industry associations. Fortune Wheel Parts’ lug nut engineering is anchored against these references.
- ASTM International (publisher of the ASTM B117 salt-spray test standard and the ASTM A563 mechanical-property specifications for carbon and alloy steel nuts)
- SAE International (publisher of SAE J429 / J1199 mechanical-property and proof-load standards for fasteners, and SAE J1739 for fastener torque validation)
- ISO 9001 — Quality Management Systems (International Organization for Standardization)
- ISO 16047 — Fasteners — Torque-Clamp Force Testing (International Organization for Standardization)
- ISO 6503 — Metallic and Other Inorganic Coatings — Corrosion Protection of Steel and Aluminum (International Organization for Standardization)
- ASTM G1 / G4 — Standard Practices for Preparing, Cleaning, and Evaluating Corrosion Test Specimens and Galvanic Compatibility (ASTM International)
- SEMA (Specialty Equipment Market Association) (publisher of the SEMA wheel-fitment and lug-nut interchangeability guidance for the North American aftermarket)
Bobby
Manager · Ningbo Fortune Auto Parts Manufacture Co., Ltd. (Fortune Wheel Parts)
Bobby manages the Fortune Wheel Parts wheel-fastener program. The company was founded in 1996 in Ningbo and is one of the leading professional manufacturers of wheel balance weights, tire valves, and tool accessories. Fortune’s wheel lug nut range covers ACORN, BULGE ACORN, DUALIE ACORN, MG-ATTACHED WASHER, OPEN-END, and lug bolt configurations, with the racing-car 2PC BULGE ACORN range built around the 60 degree conical seat standard. Reach the team at fortunewheelparts.com/contact-us or sales@fycautoparts.com. Find us on LinkedIn, Facebook, and YouTube.
Post time: Oct-08-2026